Laboratory Check
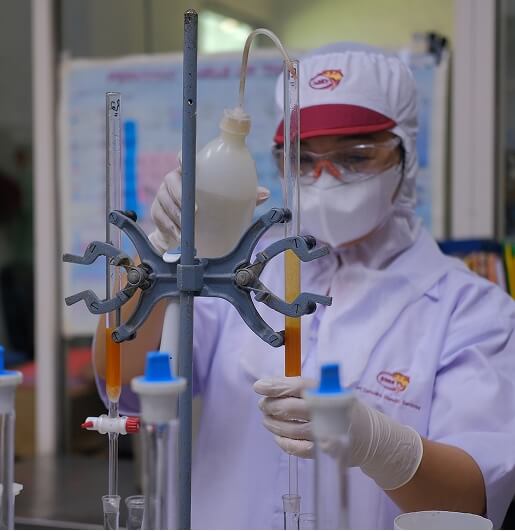
Bacterium checking process in all production equipment, water that will be used and employee hygiene so that the produced product’s quality is guaranteed.

Receiving
Place for reception and inspection of raw materials to inspect its histamin content, and removal of fish entrails.

Quality Inspection
Analyzing histamin content of the fish, salt, oil and vegetables that will be used in production process to produce tuna can product that have good quality and good to be consume.
Pre-Cooking
Temperature and cooking time should correspond to the size of the fish to remove its remaining oil and body fluids, and to simplify loin process that easily removed from its backbone.

Loining
-
Loining is performed manually to separate the meat from backbone and other cleaning defects such as black meat and bones
-
Loining is done as quickly as possible
-
The loins are checked by QC Inspector

Metal Detector
-
All cleaned fish are passed through the metal detector to assure no metal contamination of the product
-
Sensitivity of metal detector is checked by QC Inspector

Packing
Fish filling is done by packshaper machine and then weighted. Filing weight and net weight control is done by Quality Control inspector.

Seaming
Seaming is done by seaming machine automatically and cans should be washed after the seaming process.

Retorting
-
The process, equipment, temperature, time and monitoring records are approved by a process authority.
-
The temperature and time of sterilization is monitored and recorded by QC Inspector.

Labelling
-
Prior to labeling, the finished goods are examined to remove defective, rusty, dirty, or damaged cans.
-
All cans are labeled bearing the country of origin, brand, name of product, net weight, expiry date, nutrition facts, etc.

Stuffing
-
The container is clean, dry, and completely sealed to protect products from water, dust, dirt, and other foreign matter.
-
Stuffing is done carefully to prevent product from acquiring physical damage
-
Cartons are arranged in interlocking position to minimize movement of product while in transit

Ice Plant
-
High-Capacity Ice Production: Equipped with an in-house ice plant capable of producing 100 Metric Tons (MT) of ice per day to ensure a continuous and reliable cold supply.
-
Temperature Control & Freshness: Ice is immediately utilized during raw material receiving and processing to maintain optimal cold-chain temperatures and preserve fish quality.
-
Hygienic Standards: Produced under strict food safety and hygiene controls, ensuring zero contamination before the ice touches the raw fish.

Cold Storage
-
3,000 MT Total Capacity: Our high-volume cold storage facility accommodates up to 3,000 MT, allowing us to store raw materials and finished goods reliably.
-
4 Dedicated Storage Rooms: Divided into 4 separate controlled chambers to optimize temperature management, organized inventory flow, and product segregation.
-
Cold-Chain Integrity: Maintains consistent, deep-freeze temperatures to preserve fish quality, safety, and shelf life before export.
